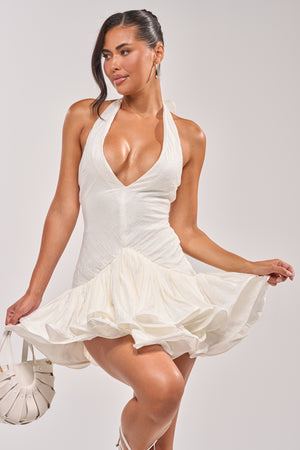
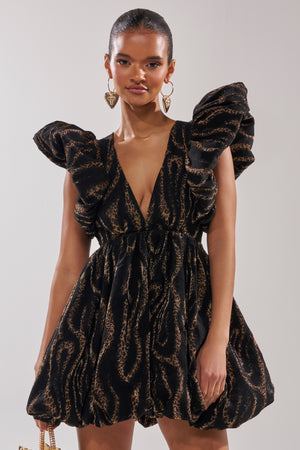
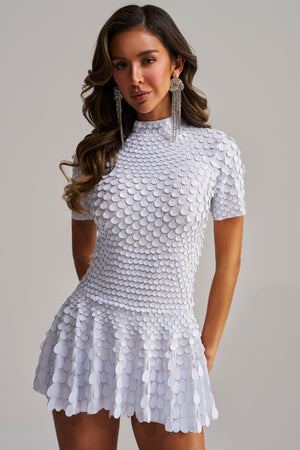
Modern Transparent Button in Ribbed Jersey with Monogram Hardware
Source:Transparent Button /
Time:2026-09-30
Modern Transparent Button in Ribbed Jersey with Monogram Hardware
A Hotel Group approached us to develop a modern transparent button around a single idea: monogram hardware, executed in ribbed jersey. The capsule was destined for Czechia and needed modern finishing that reads designer on the rail while staying repeatable in bulk. This case study records the brief, the specification and the delivery.
The challenge
- Decoration durability failed after two washes
- Unit costs were too high for a boutique price point
- Delivery missed the collection launch window

What we specified
| Product | Modern Transparent Button |
|---|---|
| Client type | A Hotel Group |
| Market | Czechia |
| Order volume | 600 pieces across 5 colourways |
| Base material | Ribbed Jersey |
| Signature detail | Monogram Hardware |
| Size range | 0-14 |
| Sampling rounds | 4 |
| Delivery window | 6 weeks from PO to ex-factory |
| Compliance | WRAP |
How it was built
- Reference garments and moodboards were translated into a measurement spec, not just photos.
- Ribbed Jersey was confirmed with lab dips and a hand-feel approval before grading.
- The transparent button was prototyped on the fit model, then revised twice before pre-production.
- Monogram Hardware was applied in a controlled process to keep every piece consistent.
- Bulk ran with in-line inspection; a photo report was shared before shipment.

Result
- 600 pieces delivered inside the 6-week window.
- Unit cost held within 3.0% of the approved quotation.
- The a Hotel Group launched on schedule and reordered the same specification next season.
What we would repeat
Keep one process owner on both sides. Most delays come from hand-offs, not machines.

Planning a similar capsule?
Send us your tech pack or even a rough sketch — we will come back with fabric options, a costed sample plan and a realistic production calendar.